Ethanol Fuel Production Explained: Manufacturing Processes, Blending Technologies & Fuel Quality Insights
Ethanol fuel is an alcohol-based fuel produced from biological materials such as sugarcane, corn, grains, and agricultural residues. It is commonly used as a blending component in petrol and plays an important role in renewable energy research.
Ethanol has the chemical formula C₂H₅OH. Its properties influence fuel combustion, engine performance, and the characteristics of petrol blends. However, its overall environmental impact depends on the raw materials, manufacturing methods, energy consumption, transportation, and final application.
Ethanol fuel production combines agricultural processing, fermentation, distillation, dehydration, laboratory testing, and controlled blending. Each stage influences the quality, purity, and suitability of the finished fuel.
What Is Ethanol Fuel?
Ethanol fuel is ethanol prepared according to the requirements of a particular fuel application. It differs from beverage alcohol because fuel-grade ethanol is manufactured and tested for industrial use. Depending on the application and local regulations, it may also contain approved denaturing agents.
Important characteristics include:
Octane rating: Ethanol has a high octane rating and can improve a petrol blend's resistance to engine knocking.
Oxygen content: Ethanol contains oxygen, which influences combustion characteristics.
Energy content: Ethanol contains less energy per litre than conventional petrol, so fuel economy can change depending on the blend and engine.
Water absorption: Ethanol readily absorbs water, making moisture control important during production and storage.
Material compatibility: Higher ethanol concentrations may require compatible fuel-system components and specially designed engines.
Why Ethanol Fuel Production Matters
Ethanol production connects agriculture, industrial manufacturing, transportation, and energy policy.
Renewable raw materials
Sugar-containing crops, starch-rich grains, and selected agricultural residues can be converted into ethanol. Using suitable feedstocks can create additional uses for agricultural materials, depending on local resource availability and environmental considerations.
Fuel diversification
Blending ethanol with petrol introduces another component into the transport fuel supply. Domestic ethanol production can help diversify energy sources in regions with appropriate agricultural and manufacturing infrastructure.
Agricultural development
Ethanol facilities create demand for suitable agricultural raw materials. Sugarcane-processing regions may also use molasses, a by-product of sugar manufacturing, as a feedstock.
Environmental considerations
Ethanol can influence vehicle emissions, but the outcome depends on the fuel blend, engine design, and operating conditions. A complete environmental assessment also considers farming, fertilizers, processing energy, transportation, and land-use changes.
Major Raw Materials Used in Ethanol Production
The raw material determines how sugars are obtained and influences the complexity, energy requirements, and efficiency of the production process.
1. Sugarcane Juice and Molasses
Sugarcane contains fermentable sugars that microorganisms can convert into ethanol. Sugarcane juice can be processed directly, while molasses provides another sugar-rich raw material.
The general process includes juice extraction or molasses preparation, fermentation, distillation, dehydration, and quality testing.
Sugarcane-based ethanol production is particularly relevant in countries with established sugar industries, including Brazil and India.
2. Corn and Other Starch-Rich Grains
Corn, wheat, and other grains contain starch that must be converted into simpler sugars before fermentation.
The process generally involves milling, liquefaction, saccharification, fermentation, distillation, and dehydration.
Remaining grain solids may be processed into animal-feed ingredients where the production system and applicable requirements permit.
3. Other Sugar-Rich Crops
Sugar beet, sweet sorghum, and other suitable crops can provide fermentable sugars. Their suitability depends on climate, agricultural productivity, seasonal availability, and local processing infrastructure.
4. Agricultural and Forestry Residues
Plant residues contain cellulose and hemicellulose, which can be converted into fermentable sugars. This process is commonly associated with cellulosic ethanol production.
Typical stages include pretreatment, sugar conversion, fermentation, and product recovery.
Cellulosic ethanol can expand the range of available raw materials, but its production involves challenges such as pretreatment energy requirements, enzyme performance, fermentation inhibitors, and process integration.
Main Stages of Ethanol Fuel Manufacturing
Conventional ethanol production generally follows a sequence of raw-material preparation, sugar conversion, fermentation, distillation, dehydration, quality testing, and blending.
1. Raw Material Preparation
Raw materials are prepared to make their fermentable components accessible.
Sugarcane is crushed or pressed to extract juice. Molasses may be diluted and adjusted to provide a suitable fermentation mixture. Grains are cleaned and milled to improve processing efficiency.
Agricultural residues may require size reduction and additional preparation before further processing.
Proper preparation helps improve conversion efficiency and reduces difficulties during subsequent manufacturing stages.
2. Sugar Conversion
The sugar-conversion stage depends on the type of raw material.
Sugarcane juice and molasses already contain fermentable sugars, although their composition may require adjustment. Starch-based materials need additional processing.
In grain-based production, enzymes break starch into smaller carbohydrates. Liquefaction reduces starch viscosity, while saccharification produces sugars that yeast can ferment.
Cellulosic materials require pretreatment to open up the plant structure. Enzymes or other conversion methods then release sugars from cellulose and hemicellulose.
The objective is to produce a suitable mixture for fermentation while controlling substances that could inhibit microorganisms.
3. Fermentation
Fermentation is the biological stage in which microorganisms convert fermentable sugars into ethanol and carbon dioxide.
Selected yeast strains, particularly Saccharomyces cerevisiae, are widely used in conventional ethanol production.
Important factors affecting fermentation include:
Sugar concentration
Temperature and acidity
Yeast strain and health
Nutrient availability
Contamination control
Fermentation duration
Inhibitory substances in the raw material
Fermentation may operate in batch, fed-batch, or continuous systems. Each approach has different requirements for equipment, process monitoring, and production management.
The resulting liquid contains ethanol, water, residual sugars, yeast, and other substances. Additional separation is required to obtain fuel-grade ethanol.
4. Distillation
Distillation separates ethanol from much of the water and other components in the fermented liquid.
Industrial facilities use distillation columns or integrated separation systems to concentrate ethanol. Heat recovery can reduce energy consumption by transferring heat between different parts of the process.
Ordinary distillation cannot completely remove water because ethanol and water form an azeotrope under standard operating conditions. Additional dehydration is therefore necessary when the intended fuel specification requires very low water content.
5. Dehydration
Dehydration removes additional water from concentrated ethanol.
Molecular-sieve adsorption is a widely used industrial method. It uses a porous material that selectively retains water, allowing ethanol to reach a higher level of dryness.
Other separation methods may be used depending on plant design and operating requirements.
Dehydration is important because excess water can create storage and handling problems when ethanol is blended with petrol.
6. Final Conditioning and Storage
After separation, ethanol undergoes final conditioning according to its intended application and applicable specifications.
The finished product is stored in compatible tanks with controls for moisture, contamination, and material compatibility. Storage systems must also account for ethanol's flammability and vapour hazards.
Fuel-grade ethanol may be subject to denaturing requirements depending on local regulations and its intended use.
7. Quality Testing
Before distribution, ethanol is tested against the specification applicable to its intended use.
Testing may include ethanol concentration, water content, acidity, inorganic contaminants, appearance, and other relevant characteristics.
Quality management continues beyond the production plant. Sampling procedures, tank management, transportation, and blending operations can all affect the quality of the finished fuel.
Ethanol Production Methods Compared
Production method | Main raw material | Key process | Main consideration |
|---|---|---|---|
Sugar-based | Sugarcane juice and molasses | Sugar fermentation | Can use existing sugar-processing infrastructure |
Starch-based | Corn, wheat, and other grains | Starch conversion and fermentation | Requires enzymatic processing |
Cellulosic | Agricultural and forestry residues | Pretreatment and sugar conversion | More complex processing requirements |
Other sugar crops | Sugar beet and sweet sorghum | Sugar extraction and fermentation | Depends on crop suitability and seasonal supply |
Ethanol Blending Technologies
Ethanol blending combines fuel-grade ethanol with petrol at a specified proportion. Blend designations generally indicate the ethanol percentage by volume, subject to the definitions and requirements of the relevant market.
E5 and E10
E5 contains approximately 5% ethanol by volume, while E10 contains approximately 10%.
These blends are used in several markets, subject to local fuel specifications and vehicle compatibility. Manufacturer recommendations should always be checked before selecting a fuel blend.
E20
E20 contains approximately 20% ethanol by volume.
Its suitability depends on engine design, fuel-system materials, manufacturer guidance, and applicable fuel requirements. Higher ethanol proportions can affect cold-start behaviour, fuel calibration, material compatibility, and energy content.
E85 and Other High-Ethanol Blends
E85 is a high-ethanol fuel designation commonly associated with flex-fuel vehicles in certain markets. Its exact ethanol content can vary according to regional specifications and seasonal requirements.
Vehicles designed for high-ethanol blends use compatible materials and engine controls. Conventional petrol vehicles should not be assumed to support these blends.
How Ethanol Is Blended with Petrol
Ethanol and petrol may be blended at approved terminals or other suitable facilities using controlled measurement and mixing equipment.
In-Line Blending
Ethanol and petrol enter a flowing fuel stream at controlled rates. Properly designed systems monitor flow, blend proportions, and other relevant parameters.
Batch Blending
Specified quantities of ethanol and petrol are combined in a tank or mixing system. The finished batch is tested to confirm that it meets the intended specification.
Automated Blending and Monitoring
Modern facilities can use flow meters, control systems, automated valves, and sampling arrangements to maintain the required blend proportions.
Blending systems must account for moisture, fuel composition, temperature-related measurement effects, and the quality requirements of the finished fuel.
Fuel Quality Parameters
Fuel quality determines whether ethanol and the finished blend are appropriate for the intended application.
Ethanol Content
Ethanol concentration is measured to confirm compliance with the applicable specification. Requirements differ between fuel-grade ethanol and finished petrol blends.
Water Content
Excess water can create storage and handling difficulties. Under certain conditions, water in ethanol-petrol blends can cause phase separation, in which the mixture separates into distinct liquid phases.
Acidity
Acidic impurities may contribute to corrosion or indicate contamination during production. Acidity is therefore controlled according to the applicable fuel specification.
Methanol and Other Impurities
Unwanted alcohols, residual organic compounds, and other contaminants can affect fuel suitability. Permitted levels depend on the intended application and relevant standards.
Inorganic Contaminants
Certain inorganic compounds may contribute to corrosion or other operational problems. Monitoring helps maintain product quality throughout manufacturing and distribution.
Appearance and Contamination
Visual inspection can identify unusual haze, suspended particles, or signs of contamination. However, appearance alone cannot confirm compliance with a fuel specification.
Finished Fuel Properties
The final petrol-ethanol blend must meet its own requirements. Relevant properties may include vapour pressure, volatility, octane rating, water tolerance, and other regulated characteristics.
Equipment Used in Ethanol Production Plants
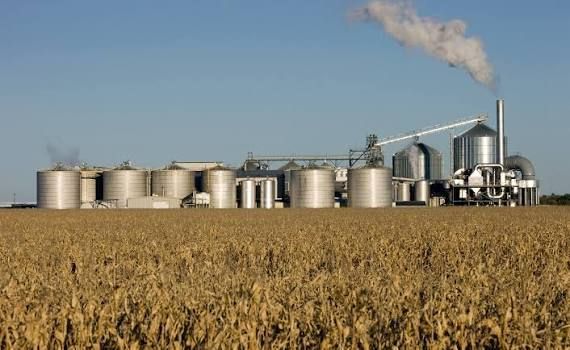
Ethanol manufacturing facilities combine equipment for raw-material preparation, fermentation, separation, utilities, and product handling.
Feedstock handling equipment: Receives, cleans, stores, and transports raw materials.
Milling equipment: Reduces particle size and improves access to fermentable components.
Enzymatic processing systems: Convert starch or prepared biomass into fermentable sugars where required.
Fermentation tanks: Maintain suitable conditions for microbial activity.
Distillation columns: Concentrate ethanol from fermented liquid.
Dehydration systems: Remove residual water from concentrated ethanol.
Heat exchangers and boilers: Supply and recover thermal energy.
Pumps and pipelines: Transfer process liquids and finished products.
Laboratory instruments: Measure ethanol concentration, moisture, acidity, and other quality indicators.
Control and safety systems: Monitor temperature, pressure, flow, vapour hazards, and equipment conditions.
Equipment selection depends on production capacity, raw-material characteristics, plant design, energy availability, and applicable safety requirements.
Environmental and Energy Considerations
Ethanol is often described as a renewable fuel, but its environmental performance must be evaluated across the complete production lifecycle.
Greenhouse Gas Emissions
Lifecycle assessments consider emissions from agriculture, fertilizer use, processing energy, transportation, distribution, and fuel combustion.
A facility using low-carbon energy may have a different emissions profile from one that relies heavily on fossil fuels.
Water Use
Water is used in raw-material preparation, fermentation, cooling, cleaning, and other industrial operations. Water recycling and efficient process design can help reduce demand on local water resources.
Land Use and Agricultural Inputs
Crop-based ethanol depends on land, soil, fertilizers, and agricultural practices. Changes in land use can influence overall environmental performance.
Wastewater and By-Products
Ethanol production can generate wastewater containing organic matter and other substances that require appropriate treatment. Some facilities recover energy from suitable organic residues or use by-products in other processes when technically and legally appropriate.
Energy Efficiency
Distillation and dehydration require thermal energy. Heat recovery, efficient separation systems, improved boilers, and process monitoring can reduce energy demand.
Safety Considerations in Ethanol Manufacturing
Ethanol is flammable, and its vapours can create fire or explosion hazards under suitable conditions. Safe operations require engineering controls, trained personnel, and compliance with relevant regulations.
Important safety measures include:
Appropriate ventilation and vapour management
Equipment designed for the relevant hazardous environment
Grounding and bonding where required to control static electricity
Suitable electrical equipment
Fire detection and suppression systems
Leak prevention and spill containment
Controlled storage and transfer procedures
Personal protective equipment and emergency training
Ethanol plants also use hot liquids, steam, pressurized equipment, and industrial machinery. Safety assessments should cover the entire production process.
Ethanol Fuel Production in India
India has developed ethanol blending as part of its transport-energy and agricultural policy. The programme has encouraged the use of suitable sugar-based and grain-based feedstocks, subject to applicable rules and resource availability.
Important considerations include:
Agricultural raw-material supply and seasonal availability
Ethanol production capacity and distribution infrastructure
Petrol-blending targets and implementation requirements
Fuel quality specifications
Vehicle compatibility and manufacturer guidance
Water and energy use in industrial facilities
Regulation of manufacturing, storage, transportation, and blending
Policy targets and implementation schedules may change. Current information should be verified through relevant Indian authorities, including the Ministry of Petroleum and Natural Gas and the Bureau of Indian Standards.
Recent Technology Trends in Ethanol Production
Ethanol manufacturing continues to evolve as researchers and industrial operators seek better process efficiency, broader raw-material options, and stronger quality management.
Improved Enzymes and Fermentation
Research into enzymes, yeast strains, and fermentation conditions aims to improve conversion efficiency. Results depend on the raw material and operating environment.
Cellulosic Ethanol Development
Cellulosic production aims to convert agricultural residues and other plant materials into ethanol. Research focuses on improving pretreatment, reducing enzyme requirements, managing fermentation inhibitors, and integrating processing stages.
Energy Integration
Heat recovery and improved distillation configurations can reduce energy demand. Digital monitoring can help identify process variation and equipment inefficiencies.
Digital Quality Management
Automated sampling, calibrated sensors, laboratory information systems, and production records can strengthen traceability and help identify deviations earlier.
Diversification of Raw Materials
Agricultural residues and other non-food biomass are being studied as additional raw materials. Their practical suitability depends on collection, transportation, conversion technology, environmental impact, and competing uses.
The maturity of these developments varies. Research findings and pilot demonstrations do not necessarily indicate widespread commercial adoption.
Laws, Standards, and Regulatory Considerations
Ethanol fuel production is subject to requirements that vary by country and intended application. Regulations may cover manufacturing permits, industrial safety, environmental protection, fuel quality, storage, transportation, denaturing, and blending.
In India, relevant areas include:
Fuel quality: Applicable Bureau of Indian Standards specifications establish requirements for ethanol and finished fuel blends.
Petroleum regulation: Relevant central and state authorities oversee different aspects of fuel blending, storage, and distribution.
Environmental compliance: Industrial facilities may require approvals related to emissions, wastewater, and waste management.
Factory and fire safety: Facilities must comply with the safety rules applicable to their processes and materials.
Alcohol-related rules: Manufacturing, possession, transportation, and denaturing requirements can vary according to the product and jurisdiction.
Technical standards and regulations can be revised. Manufacturers and researchers should consult current official documents before making compliance decisions.
Tools and Resources for Learning
People studying ethanol fuel production can explore several types of technical resources.
Government energy publications: Provide information on national blending programmes and renewable fuel policies.
Fuel quality standards: Explain technical requirements and test methods for ethanol and petrol blends.
Industrial biotechnology textbooks: Cover fermentation, enzyme activity, raw-material conversion, and process control.
Chemical engineering references: Explain distillation, dehydration, heat integration, and process design.
Environmental assessment studies: Compare greenhouse gas emissions, water use, and land-use impacts.
Industrial safety guidance: Covers flammable-liquid handling, process hazards, fire prevention, and emergency planning.
Scientific journals: Present research on cellulosic conversion, fermentation systems, separation technologies, and improved enzymes.
When reviewing technical information, check its publication date, geographic scope, production method, and whether the findings come from laboratory research, pilot-scale work, or commercial facilities.
Frequently Asked Questions
1. What are the main raw materials used to produce ethanol fuel?
Common raw materials include sugarcane juice, molasses, corn, wheat, and other sugar- or starch-rich crops. Cellulosic ethanol can use selected agricultural and forestry residues.
2. How is ethanol made from sugarcane?
Sugarcane juice or molasses is prepared for fermentation. Yeast converts the available sugars into ethanol, after which distillation concentrates the ethanol and dehydration removes additional water.
3. Why is dehydration necessary for fuel ethanol?
Dehydration reduces water content to the level required by the intended fuel specification. This helps support suitable storage, handling, and petrol blending.
4. What does E20 mean?
E20 generally refers to a petrol blend containing approximately 20% ethanol by volume. Vehicle suitability depends on manufacturer guidance and the applicable fuel specification.
5. Does ethanol always reduce greenhouse gas emissions?
No. Its lifecycle emissions depend on raw-material production, land-use effects, manufacturing energy, transportation, and other factors. The complete production pathway must be evaluated.
6. Can all petrol vehicles use high-ethanol blends?
No. Higher-ethanol blends may require engines and fuel-system materials designed for them. The vehicle manual and manufacturer guidance should be checked before using a particular blend.
7. What causes phase separation in ethanol-petrol blends?
Under certain conditions, sufficient water can cause an ethanol-petrol mixture to separate into distinct liquid phases. Temperature, fuel composition, and water content influence the likelihood of separation.
8. What is the difference between conventional and cellulosic ethanol?
Conventional ethanol commonly uses sugars or starches from crops. Cellulosic ethanol uses plant materials rich in cellulose and hemicellulose, which generally require more complex pretreatment and sugar-conversion processes.
Conclusion
Ethanol fuel production is an integrated industrial process involving raw-material preparation, sugar conversion, fermentation, distillation, dehydration, quality testing, and blending. Sugarcane, molasses, grains, and plant residues provide different opportunities and technical challenges.
Blending technologies combine ethanol with petrol at controlled proportions, while laboratory testing and process monitoring help ensure that the finished fuel meets the relevant specification. Environmental performance depends on the entire production pathway, including agriculture, energy use, water management, and transportation.
Understanding these processes provides a clearer view of ethanol's role in transportation fuels and renewable energy. Future progress will depend on reliable raw-material supply, efficient manufacturing, vehicle compatibility, safe industrial practices, and transparent environmental assessments.
Disclaimer
This article is intended for general educational and informational purposes only. It does not promote any particular brand, manufacturer, product, or commercial transaction. Technical processes, fuel specifications, vehicle compatibility requirements, and regulations may vary by location and change over time. Consult current official standards, qualified technical professionals, and relevant authorities before making operational, engineering, safety, or compliance decisions.
You May Also Like